Shanxi Jianing Forging has gathered real-world cases of wind power flange rings, ring gears, bearing rings, roller rings, and other ring landings, with a complete range of finished forging products for carbon steel, stainless steel, and alloy rings, providing reference for product selection and non-standard solutions.
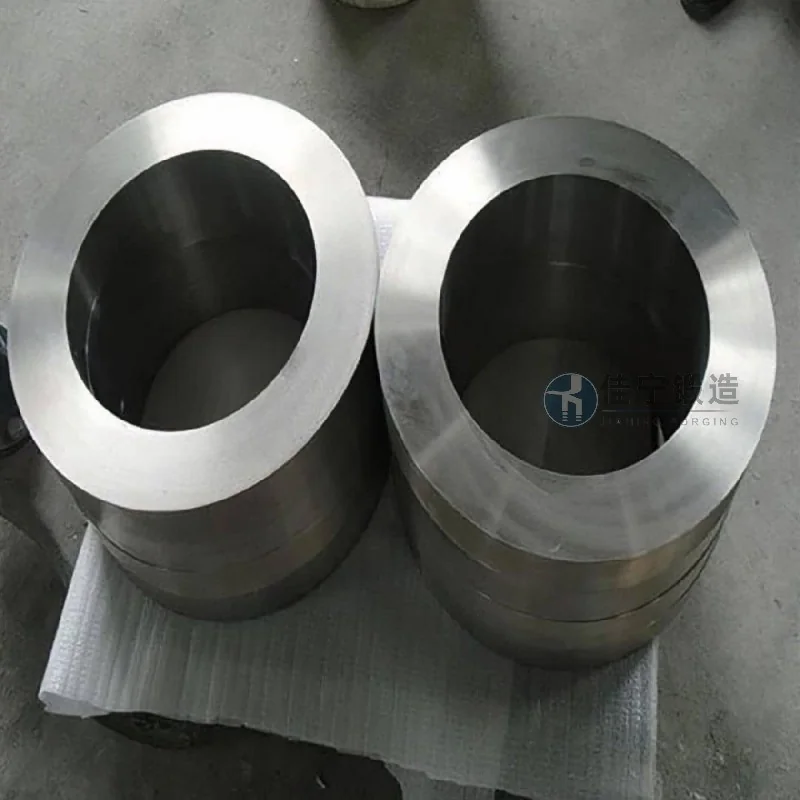
A bearing parts factory in Xinxiang, Henan, has long faced issues of unstable precision and low material utilization during the processing of ring forgings, resulting in persistently high production costs and delivery times that cannot meet downstream customer demands. The plant's original process route was relatively traditional, relying on multi-pass heating and open forging, which not only had low efficiency but also easily caused internal cracks and dimensional deviations.
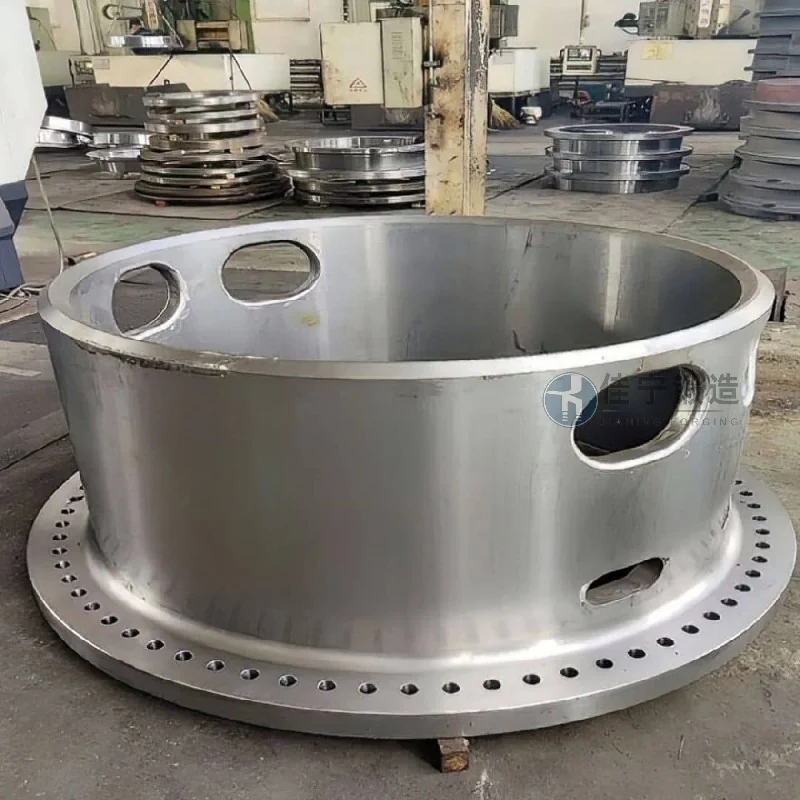
The main pain points of this bearing parts factory are concentrated in three areas: First, the finished product pass rate remains at only about 82%, with some batches scrapped due to excessive inner diameter ovality; Second, material loss is severe, with the blank weight to finished product weight ratio reaching 1.8:1, far exceeding the industry's reasonable level; Third, the processing cycle is long; a single piece needs five rounds of heating from unloading to finishing, with the entire process taking over 4 days and unable to respond to urgent orders.
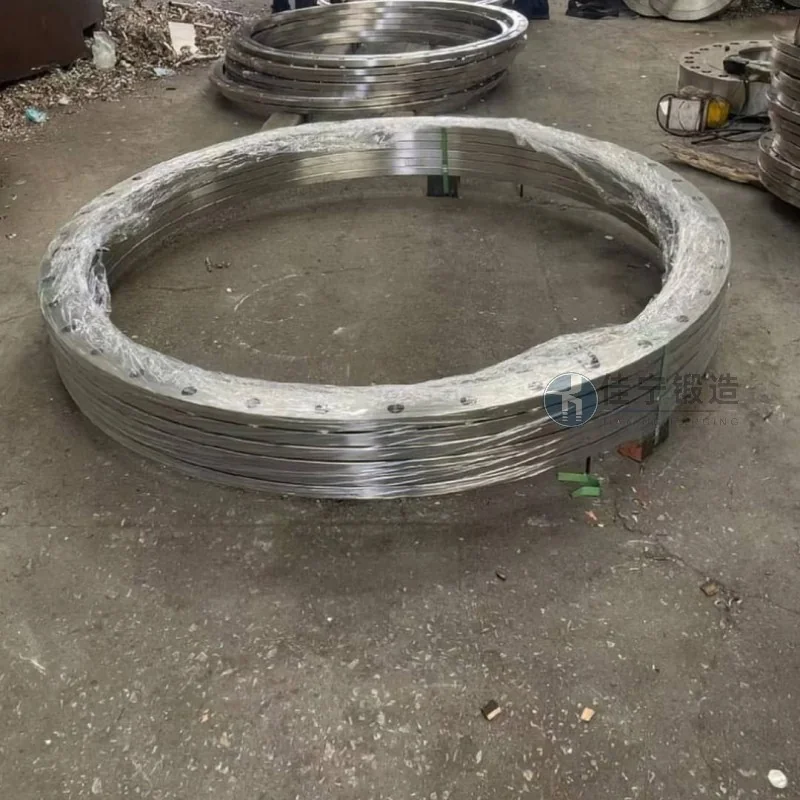
To address these pain points, Jianing Forging offers customized ring forging solutions. By adopting a fine grinding ring process combined with optimized heating specifications and mold design, the blank-to-finished product weight ratio is reduced to 1.2:1, improving material utilization. At the same time, the improved process keeps the inner diameter of the forging within 0.5mm, and the finished product pass rate remains stable above 97%. Additionally, by reducing the number of heating cycles to two and compressing the processing cycle for a single piece to 1.5 days, we effectively supported customers' delivery times.

