Shanxi Jianing Forging has gathered real-world cases of wind power flange rings, ring gears, bearing rings, roller rings, and other ring landings, with a complete range of finished forging products for carbon steel, stainless steel, and alloy rings, providing reference for product selection and non-standard solutions.
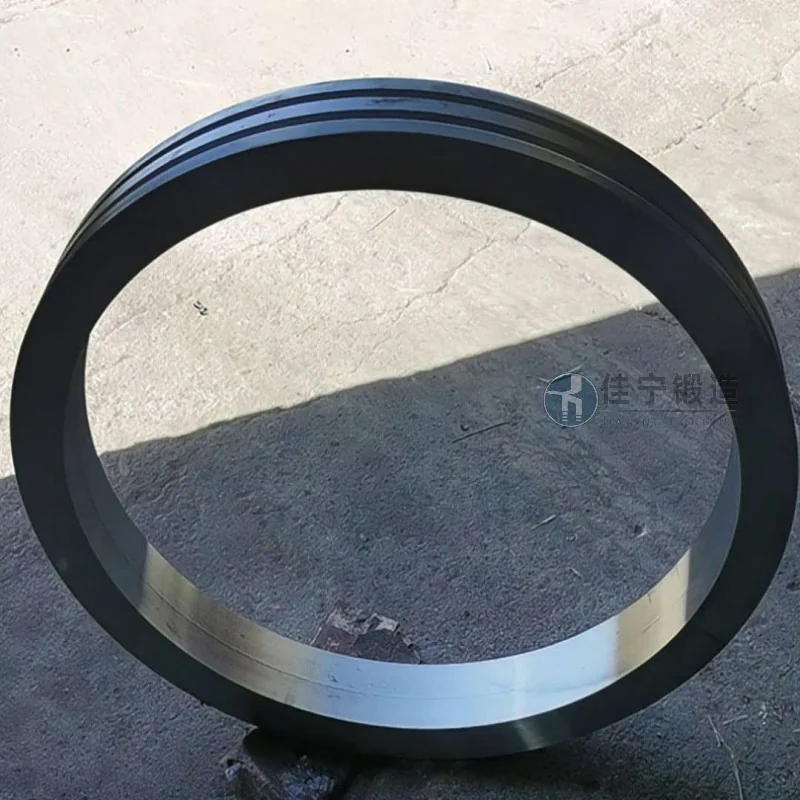
A ship machinery factory in Jiujiang, Jiangxi, needed to order a batch of high-precision ring forgings for manufacturing key connecting flanges and bearing housings when undertaking a batch of large ship transmission system components. This customer set strict requirements for dimensional tolerances, material density, and mechanical properties of the forgings, with a tight delivery schedule.
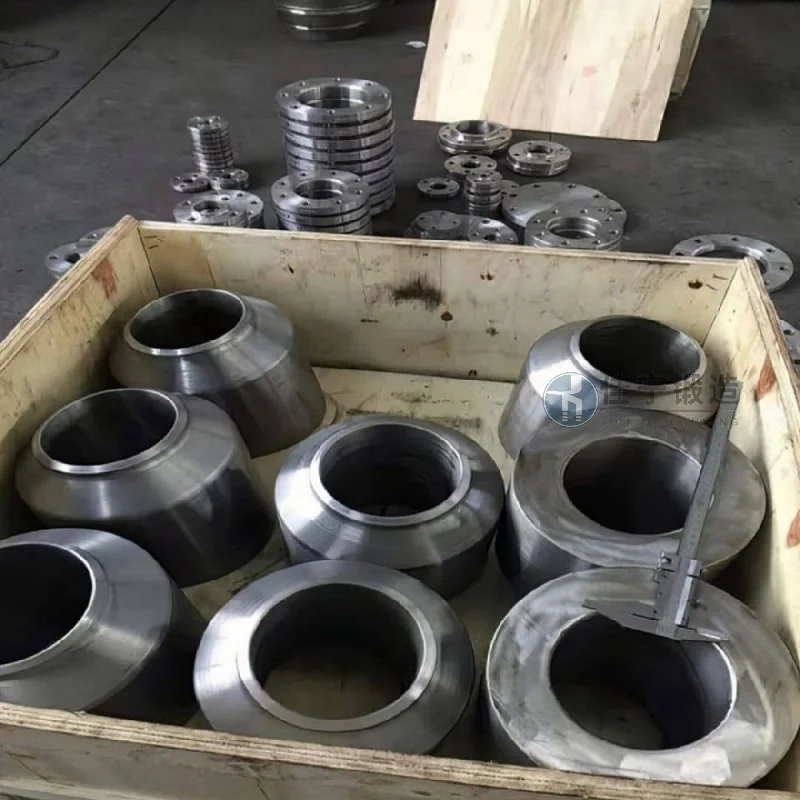
The main pain points faced by this client include:
1. Ring forgings must meet structures with diameters above 1000mm and uneven wall thickness; traditional open-die forging processes struggle to achieve coaxiality and roundness of inner and outer diameters;
2. The operating environment is marine climate, requiring materials with good corrosion resistance and low-temperature impact toughness, which ordinary forgings cannot meet standards;
3. The client has determined the project milestones and needs to complete the entire process from blank to finished product within 45 days; conventional procedures require more than 60 days.
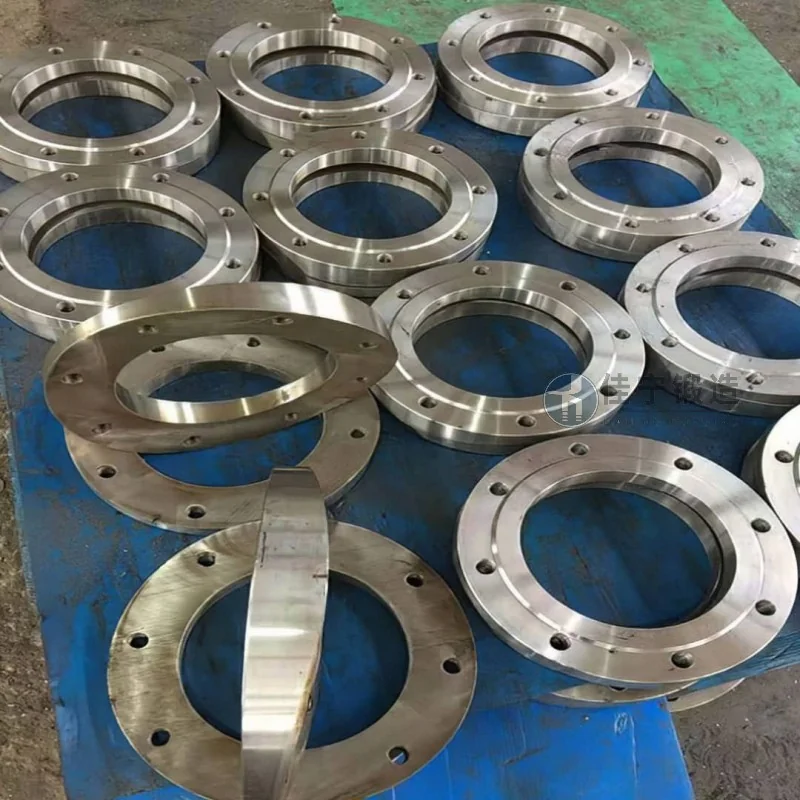
To address these pain points, Jianing Forging offers the following comprehensive solutions:
First, CNC ring rolling machines are used for fine rolling, combined with specialized special-shaped molds, to achieve one-time forming of ring forgings, with inner and outer diameter tolerances controlled within ±2mm and roundness errors less than 1.5mm;
Second, 42CrMo4 quenched and tempered steel is selected, and by optimizing the heat treatment process (quenching + high-temperature tempering), the forging's hardness is uniform (HB 260-300), with a low-temperature impact power of -20°C ≥ 40J, meeting classification society standards;
Finally, through internal production scheduling optimization and multi-process parallel operations, the production cycle was compressed to 38 days, all forgings were delivered 7 days early, and the finished product pass rate reached 1. After customer re-inspection, this batch of forgings passed acceptance in one go and has been successfully assembled into the ship's transmission system and has been operating without any issues to date.

