Shanxi Jianing Forging has gathered real-world cases of wind power flange rings, ring gears, bearing rings, roller rings, and other ring landings, with a complete range of finished forging products for carbon steel, stainless steel, and alloy rings, providing reference for product selection and non-standard solutions.
During the upgrade of key equipment, a petrochemical heavy plant in Xiamen, Fujian, set strict requirements for the performance and delivery cycle of large ring forgings. The forgings originally used by the factory frequently exhibited deformation and cracking under high temperature and high pressure, seriously affecting production continuity. To address this situation, Jianing Forging, leveraging its technical expertise in the ring forgings field, provided customized solutions.
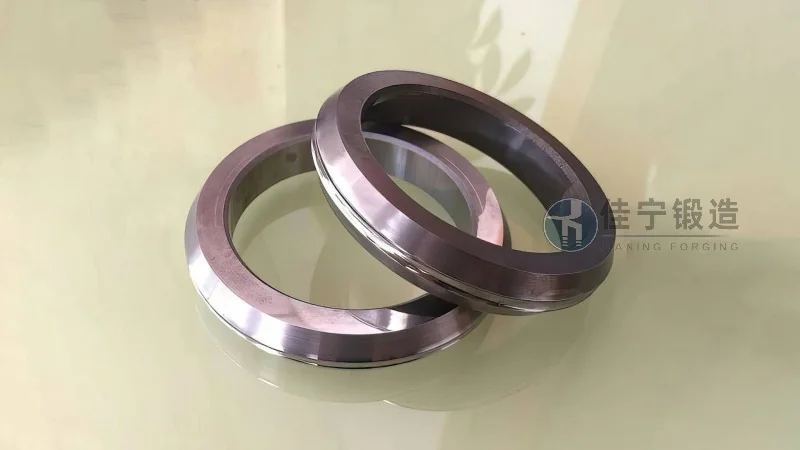
The partner for this collaboration is a petrochemical heavy factory in Xiamen, Fujian, whose core unit requires special ring forgings with an outer diameter over 2 meters and vastly different wall thicknesses. Faced with long lead times from foreign suppliers and insufficient precision from domestic peers, the factory ultimately chose to collaborate with Jianing Forging, which has many years of experience in manufacturing large forgings.
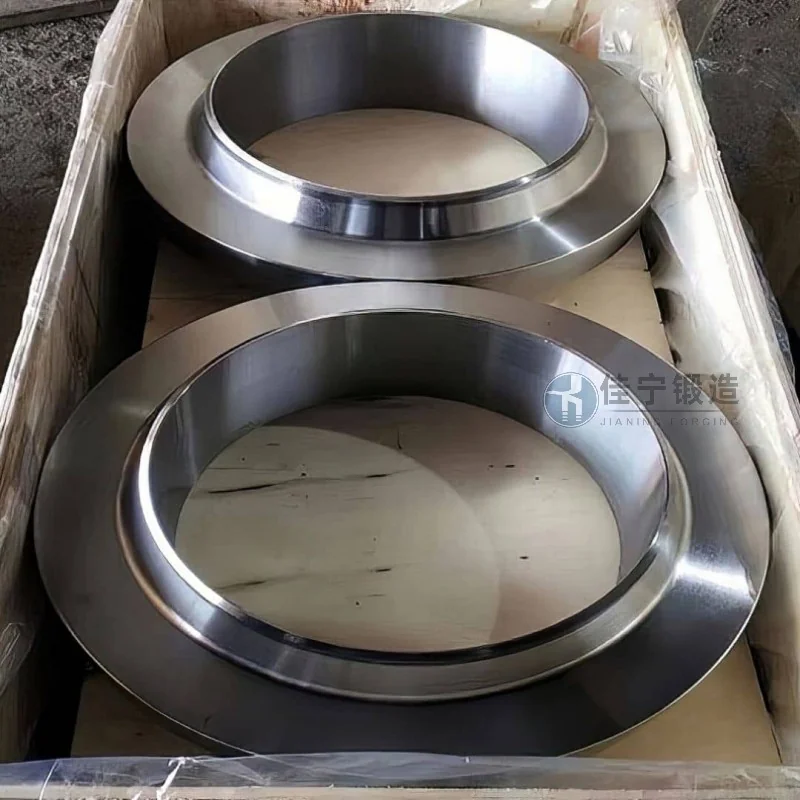
This petrochemical heavy plant faces three core challenges: First, the original forgings suffer from insufficient structural stability under long-term high temperatures (≥500°C) and high-pressure environments, resulting in local creep cracks; Second, existing suppliers cannot meet their strict dimensional tolerance requirements (concentricity deviation of inner and outer diameters must be controlled within 0.5mm); third, project schedules are tight, and the usual 90-day supply cycle cannot match the maintenance window, urgently requiring delivery within 45 days.
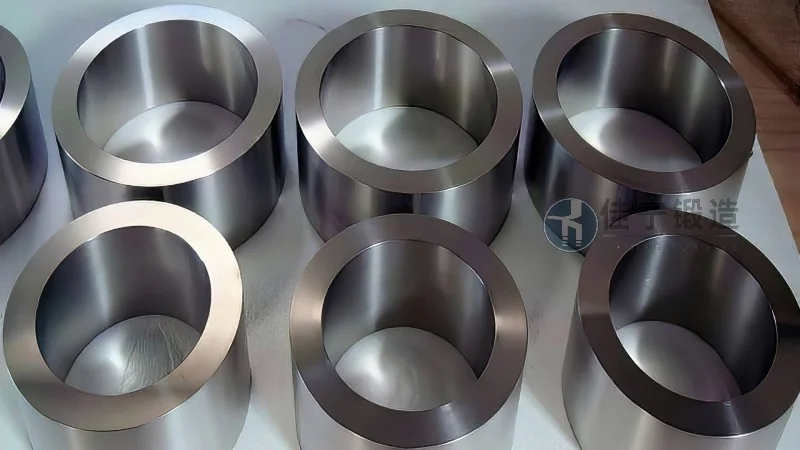
To address these pain points, Jianing Forging has systematically upgraded everything from material selection and process optimization to full-process inspection. In the material stage, specialized heat-resistant alloy steel is used, and microalloying treatment enhances high-temperature creep resistance; In the forming process, multi-heat controlled rolling technology is introduced, effectively eliminating internal stress and helping to achieve structural uniformity; At the same time, CNC ring rolling equipment is used to achieve high-precision dimensional control, with the final product's inner and outer diameter concentricity stabilized within 0.3mm. In terms of delivery, by shortening the construction period through parallel engineering, all forgings were delivered and accepted one week ahead of schedule, helping the customer resume production on time.

